
LSR Robots vs RTV Pour Labor: What Pays
LSR cycle time is often cure, not handling. A robot does not shrink vulcanization. RTV analog is mix, degas, and dump — multi-cavity trays beat a
 Kyler Yang · Founder11 min read
Automation on an LSR cell offsets labor when a person is currently doing work a machine can repeat: takeout, sprue pick, insert loading, in-line inspect, pack. It does not offset cure. Platinum LSR still needs heat and time in the cavity. A robot standing in front of a 90-second cure does not make a 90-second cure into a 20-second cure.
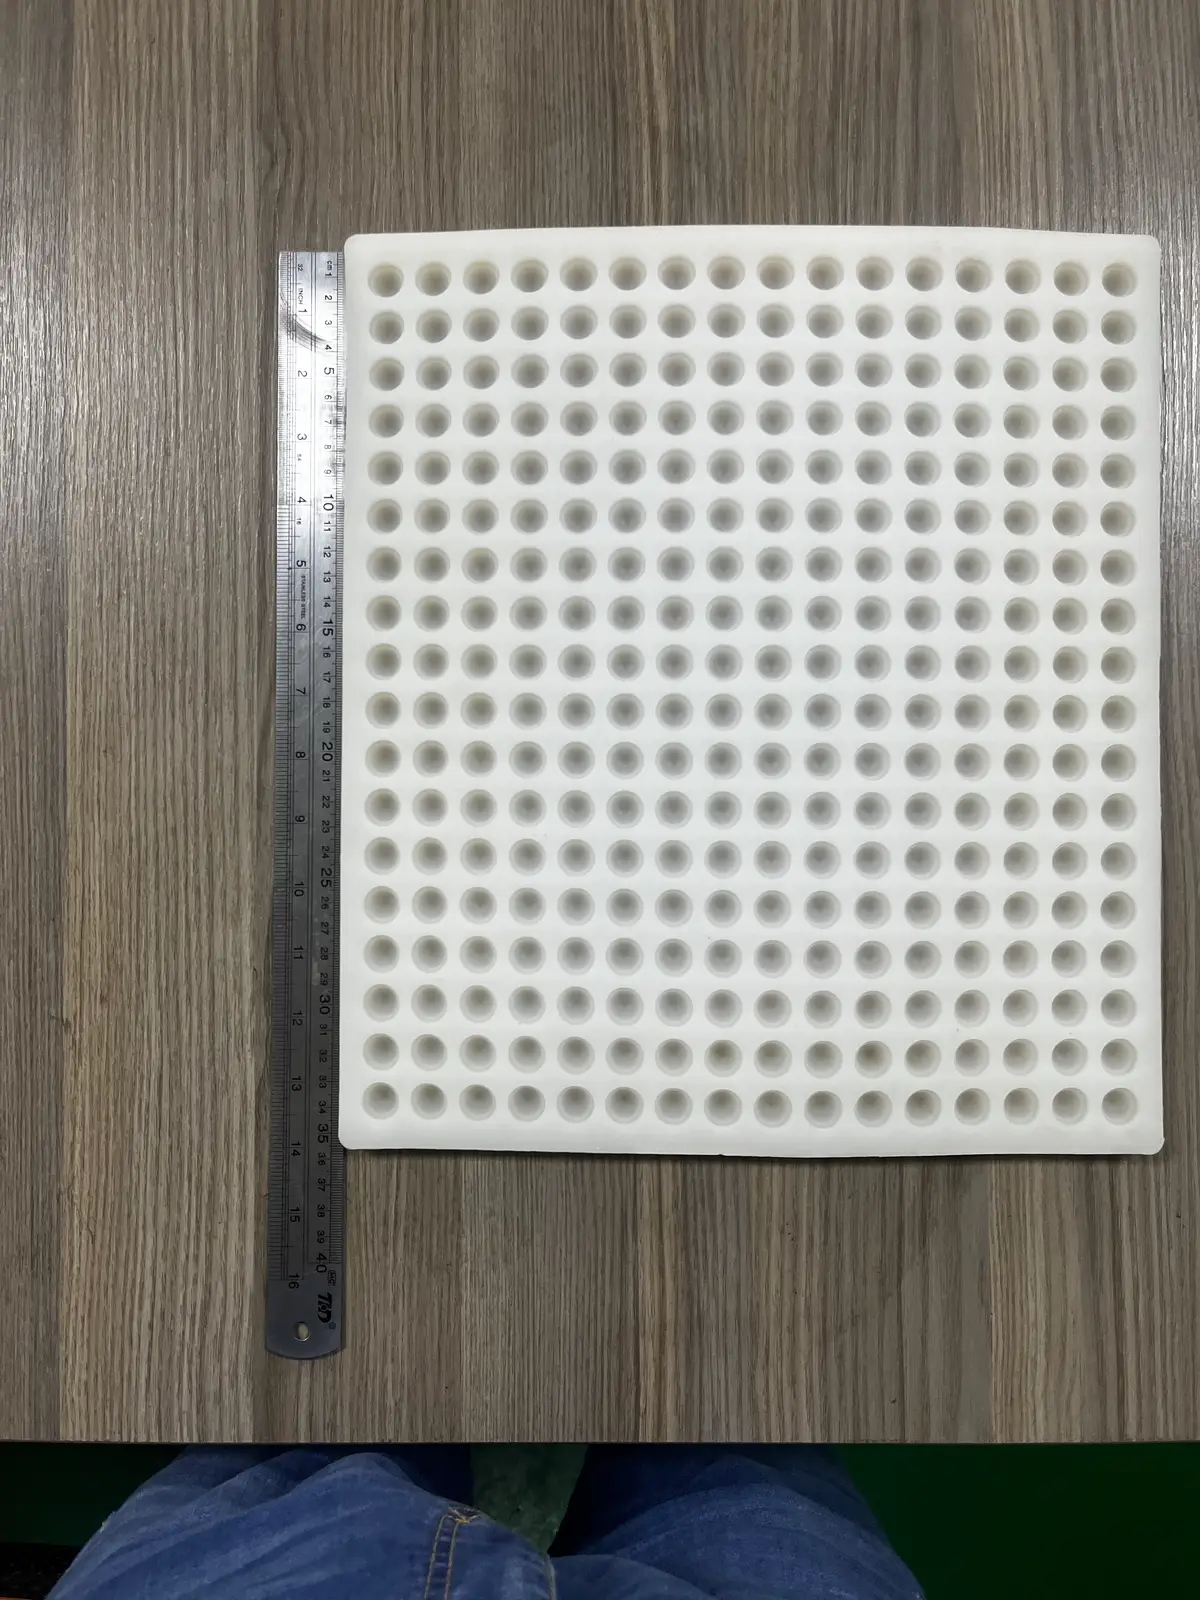
On this site the cell is a pour bench: mix A/B, vacuum degas, pour or dump, demold, pack. High-volume programs on a parts OEM buy automation to keep a multi-cavity, valve-gated tool running with one technician instead of a crowd. Low-volume custom RTV that still lives on a glove and a trimming table will not be saved by a catalog six-axis arm. Multi-cavity trays, a mix station, and a recast plan offset pour labor. A robot does not mix platinum for a 12A jacket.
Treat automation as a cell design, not as a labor percentage someone copied from a thermoplastic plant.
Where labor still sits
Map the minutes. Do not map the slogan.
At the LIM press: close, inject, cure, open. Cure dominates most parts that are not paper-thin. Labor here is tend, alarm response, drum change, and start-up. A closed-loop machine with a cold-runner already removed the “operator as mixer.” Drum kits and a meter-mix unit are the first automation most shops bought a decade ago.
At the RTV bench: weigh, mix, degas until the foam collapses, pour, wait, peel, pack. Mix and degas dominate small lots. Dump and peel dominate seasonal food trays. A closed-loop LSR meter-mix does not appear here. A scale that actually hits 1:1 or 10:1 does.
Between press/bench and carton: destage of a cured sprue or gate nub, flash trim, visual inspect, dimensional check, post-cure racking, sort, bag, label. This is where high-volume LSR still hides people. RTV hides people in trim of dump flash and in seating keys.
Inserts and overmolding: loading a plastic or metal insert every cycle is labor or it is a feeder plus a robot. Missed inserts are scrap at LSR prices. Missed pins in a pour box are helices full of platinum.
Quality theatre: 100% visual on a 64-cavity teat tool is a staffing plan. Vision and a defined AQL plus process control is a different plan. 100% photo of every gummy cavity is also a staffing plan.
If your timed cell shows 70% of labor in trim, automation that only takeouts onto a belt does nothing. If labor is one operator watching two presses, the ROI is in adding cavities or a second tool, not in a robot. If labor is one technician pouring a 1-cavity glove 6,000 times, the ROI is an 8–12 cavity tray, not a six-axis arm.
What “automation” actually is
Unbundle the quote.
Meter-mix and cold-runner. Standard on serious LSR. This is process equipment, not a labor project. It cuts wasted sprue *and* mixing labor. Count it in material and in tend time. RTV analog: a dedicated mix/degas station and kits that are not eyeballed.
Takeout robot or picker. Pulls LSR parts (and maybe the runner) every shot. Pays when: the tool is too hot or too fast for a hand to enter safely; you need consistent gate vestige; you are running lights-out; contamination control forbids a person over the cavity. Does not pay when cycle is two minutes and a person is already there packing. Does not peel a 12A jacket.
Degating fixtures. Cold-deck valve gates already minimize destage. Open sprues need a fixture or they need a person with snips. RTV: dump flash is a split problem; a robot will not seat keys.
Insert feeding. Vibratory or tray feed plus robot for overmolding. Frequently the difference between a runnable overmold cell and a job that cannot hold rate.
In-line vision / weigh / poke-yoke. Flash detection, missing insert, short shot. Pays when you would otherwise staff 100% inspect. Does not replace a capable shutoff or seated keys. Outer-row gummy weight vs center (often 3–6% heavy if the tray sags) is a jacket problem, not a camera problem.
Pack automation. Count, bag, or tray. Pays on millions of identical parts. Custom silicone with twelve SKUs a day usually still packs by hand. Seasonal dumps too.
Post-cure / wait handling. Racks that travel, ovens with recipes, no mixed lots. RTV: witness coupons, not mixed kit lots on one bench.
Depositing automation (gummy lines) is the RTV-adjacent machine people actually mean. It dumps into the cavity. It does not pour the jacket. Quote the depositing OEM separately from the mold shop.
What it offsets, and what it does not
Offsets: direct handling minutes, overtime on a cosmetic line, contamination from hands, missed inserts, destage marks, the extra person you would hire to keep a 16-cavity tool fed on third shift. On RTV: mix errors, degas time, peel time via better structure (mother first, then skin).
Does not offset: cure time, mold heat-up, siloxane price, a flashing shutoff, first-article engineering, color-change purge, overseas freight, platinum kit price, inhibition on a dirty master. A flashing 8-cavity tool plus a robot is an automated flash factory. A sagging tray plus a depositing robot is an automated weight-drift factory.
Can raise cost if mis-sized: custom EOAT for a part that will change in two months; a vision system on a texture that the camera cannot see; a robot on a 1-cavity aluminum bridge you run 400 pieces a month; a six-axis on a 1-cavity RTV glove.
Labor *rate* in a given country is a driver. Labor *content* is the other. Automation is a content play. Moving the tool to a lower-rate region is a rate play.
When labor is not the bottleneck
Cure-dominated LSR parts on a full press: buy cavities, thermal design, or a second tool before you buy a robot. The math is parts per hour at the platen.
Mix-dominated RTV: buy a scale, vacuum, and a multi-cavity jacket before you buy a robot.
Yield-dominated parts: buy shutoff, vacuum, and process window. Automating 8% scrap makes 8% scrap faster. Same for a torn 12A skin.
Changeover-dominated custom shops: buy quick-change bases, standardized cold decks, and disciplined scheduling — or standardized boxes and keys. A robot that needs a new gripper per SKU can make changeover worse.
Medical / clean: automation can be a contamination control, even when the labor hours look small. A person leaning over an ISO 7 cavity is a particle source. Here the “ROI” is the environment, not the wage line.
RUUIPON Mold Structure Decision: Labor drops when structure is right: open-back vs two-part vs core, mother so the tray does not sag. Do not automate a one-piece glove that should have been keyed.
Common mix-up: calling a cold deck “full automation”
A lot of quotes fold a manifold into a cell price. In the shop that usually means destage went away and inspect/pack did not. On RTV, calling a vacuum pump “automation” is the cousin.
What to ask when you're buying
- Timed labor minutes per 1,000 good pieces/dumps, split: tend or mix / destage or peel / inspect / pack / insert load?
- Cycle time and whether cure dominates (LSR) or mix/dump dominates (RTV)?
- Cavitation and gate type (valve vs open) — or cavity count and jacket type?
- Which minute pile each proposed device removes?
- Staffing after automation (do not accept “unmanned” if drums still change and ovens still load — or if kits still weigh)?
Worked example
You're running a 16-cavity LSR teat, valve-gated, 90 s cure, 100% visual on third shift. Time inspect/pack; that pile may want vision or a better shutoff before a takeout robot. You're also pouring a 1-cavity gummy glove 8,000 times a season. Buy an 8–12 cavity jacket and a mix station. Do not buy a six-axis for the glove.
We would not recommend a robot to shorten vulcanization
We would not recommend automating flash instead of fixing the land, a new gripper per SKU on a custom shop, or a six-axis on a 1-cavity RTV glove. We would not accept “unmanned” if drums and ovens still need people.
- Time the piles -> Largest pile?
- Largest pile? - LSR inspect/pack -> Vision or better shutoff
- Largest pile? - LSR insert load -> Feeder
- Largest pile? - LSR tend on long cure -> More cavities
- Largest pile? - RTV mix/peel -> Scale, degas, multi-cavity jacket
- Labor complaint - Robot vs 90 s cure -> Cure still owns the clock
Typical shop values
Reference values only. Confirm material-specific limits against the supplier’s technical data and agree project acceptance criteria before production.
| Item | Typical shop value | | --- | --- | | LSR cavity | About 160–200 °C; cycle often cure-dominated | | Cold deck | Valve-gated decks cut destage; they do not bag parts | | RTV mix | Platinum 1:1 or 10:1; degas until the foam collapses | | First food layout | 8–12 cavities is a common labor step-up | | Outer-row vs center if tray sags | Edge often 3–6% heavy — jacket, not a robot | | ISO 3302-1 | M2 common; automation is not a class |
Copy this into an automation RFQ
- Timed current labor minutes per 1,000 good, split by pile
- Cycle time; cavitation; gate type (LSR) or jacket type (RTV)
- Proposed devices, and which minute pile each removes
- Staffing after; changeover time with EOAT; scrap with/without vision
- Maintenance of needles, cameras, feeders (a down robot is a down press)
Send the timed piles. We'll add cavities or a mix station — not a catalog arm on a glove. Custom RTV molds.
Related: ROI RTV to LSR, 1 vs 8 cavity, gummy molds.
FAQ
Will a takeout robot shorten my LSR cycle time? Usually not in a way you will feel, because cycle is dominated by cavity heat and part thickness. A robot can shave the mold-open pause a human needs on thin, fast shots; on a thick gasket, cure still owns the clock. Buy the robot for handling, safety, and contamination, not for vulcanization. It will not pour an RTV jacket faster either.
Is automation worth it in a lower-wage factory? If labor *content* is destage and 100% cosmetic inspect on millions of parts, yes: consistency and contamination can outweigh wage. If content is one tend operator on a cure-dominated 2-cavity industrial part, no. If content is one technician on a 1-cavity glove, buy cavities. Run minutes, not country stereotypes.
Does a valve-gated cold-runner count as labor automation? It is process equipment that removes destage labor and sprue waste. Count both. It will not pick parts or bag them. Shops that call a cold deck “full automation” are selling a manifold as a cell. A vacuum pump on an RTV bench is the cousin.
What labor should I time before I approve a robot PO? Split tend, insert load, destage, inspect, pack, and post-cure handling on a normal lot — or mix, degas, pour, peel, pack on RTV. Circle the largest pile. If it is inspect, ask for vision or a better shutoff first. If it is mix, ask for a scale and a tray. Match the device to the pile.
Can automation replace process validation on medical LSR — or mix control on RTV? No. A robot is a process input. It needs its own validation: grip marks, cycle interrupt, contamination from EOAT grease, lot identity when a camera rejects a cavity. 13485 change control still applies. Automation without a validation plan is a faster unvalidated cell. RTV mix still needs a weigh and a kit lot.
Custom silicone development · DFM & prototype support
CAD, drawing, photos or sample details