
Mold Release on the Master, Not Inside the RTV Cavity
On RTV work, release belongs on the master, not in the cavity. Semi-permanent films sit on steel parts tools. Never solvent-spray a culinary pour face.
 Kyler Yang · Founder8 min read
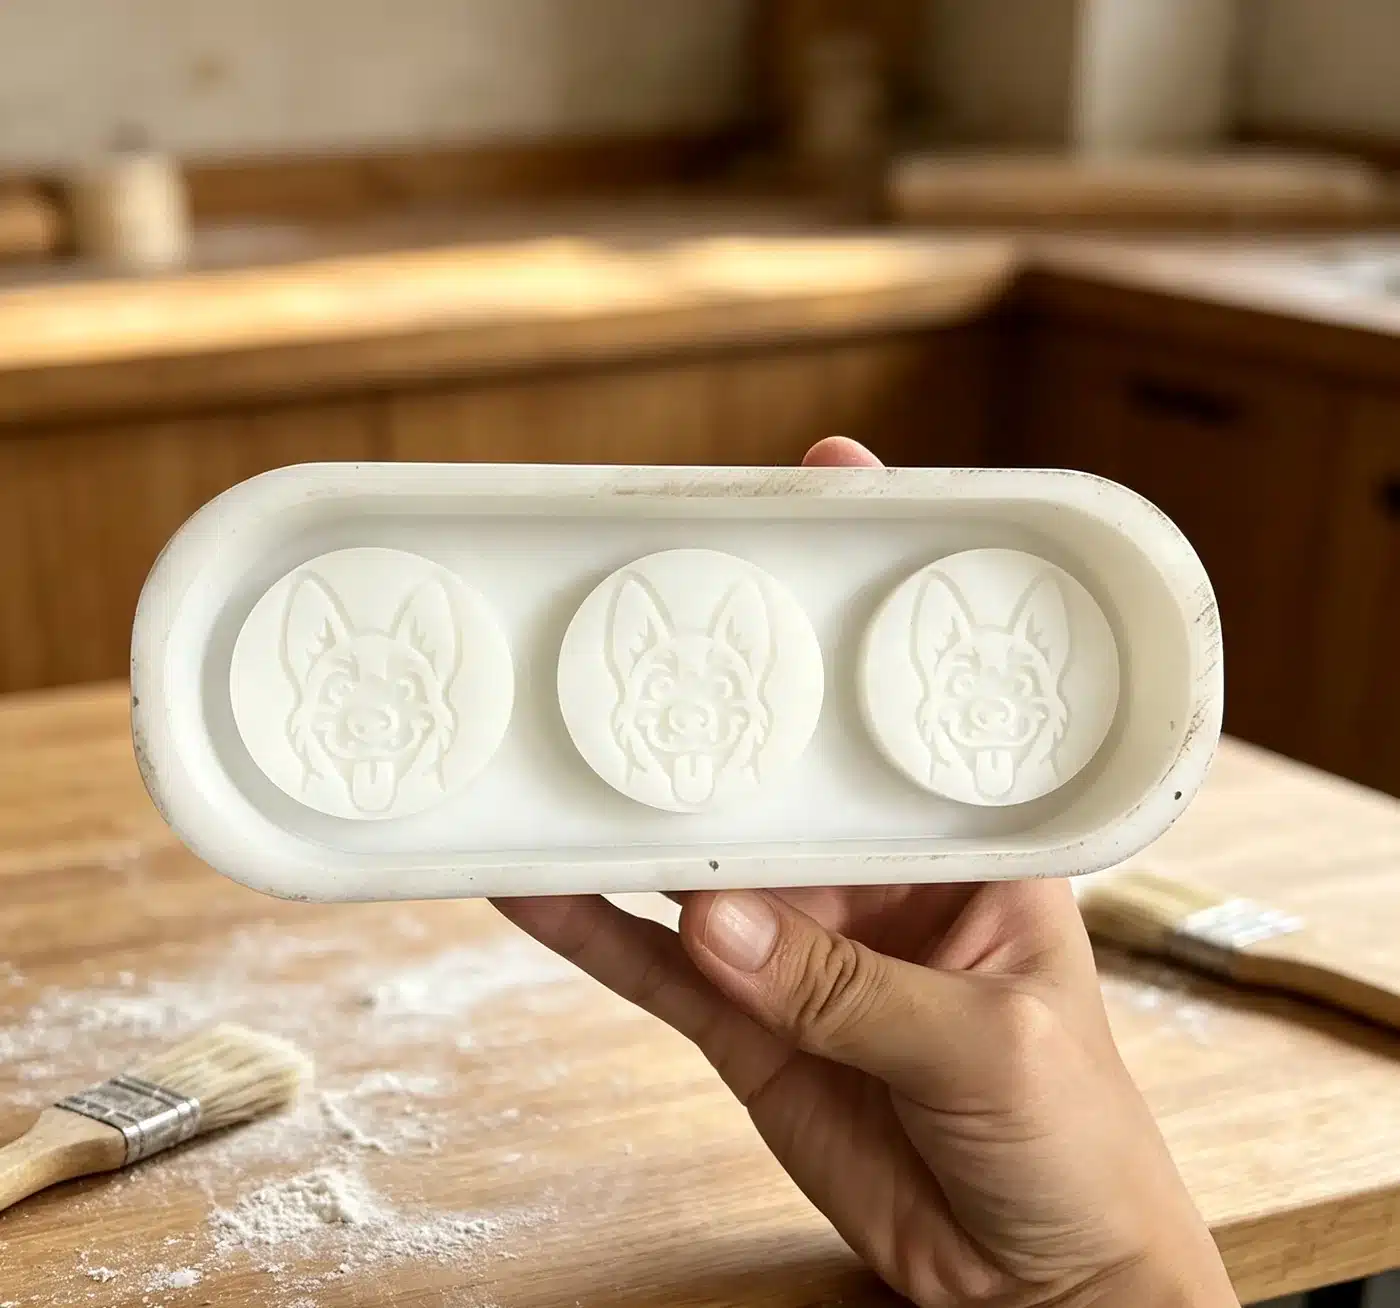
On a custom RTV mold, the release question is usually master-to-silicone, not silicone-to-silicone. Keep solvent-based sprays off the pour face. Semi-permanent coatings belong on steel *parts* tools, not inside a 10A–20A food or resin cavity.
The fork is not “which can is stronger.” It is whether the film stays on the pattern, leaves with the casting, or contaminates the rubber you just paid to pour.
Two films, two jobs — and a third object
Sacrificial / solvent-borne sprays. A carrier solvent lays down silicone oil, wax, or a resin solution. The solvent flashes. The film is a physical barrier. Each cycle can strip some of it, so you respray. Transfer onto the casting is expected. Build-up in texture is expected if you over-apply. VOC, flash fire, and inhalation are shop problems, not fine print.
Semi-permanent coatings. A reactive resin (often a cross-linking silicone or fluoropolymer system) is wiped or sprayed, then cured onto *metal*. The film is meant to bond to the tool and survive many cycles with little transfer. That is an HCR/LSR steel conversation. You cannot bake a semi-permanent film onto a platinum RTV skin and call it a jacket.
Barrier on the master (this site). For platinum or tin poured against plaster, resin, wood, or print, you want a named barrier so the master releases and so sulfur, amines, or undercured SLA do not inhibit platinum. The barrier is part of tooling, not a courtesy. Oil in the RTV mix causes fish-eyes and inhibition drama.
Water-based sacrificial emulsions exist too. They are not semi-permanent just because they are water. They still transfer. They need flash-off before the first fill, which is slow on a cold RTV bench.
Where each one belongs
| Situation | Prefer | Why | | --- | --- | --- | | Platinum/tin RTV poured on a master | Barrier on the *master*, not oil in the silicone | Oil causes fish-eyes and inhibition | | Food, chocolate, bakeware, gummy cavities | No spray in the cavity. Redesign peel or food-contact film only if the article is retested | Release is a contaminant | | Castings that will be bonded, painted, or overmolded later | No oil in the cavity | Sacrificial silicone oil wrecks adhesion | | Hot HCR/LSR into steel (different quote) | Semi-permanent on steel, or run dry | Many releases per coat; medical often wants none | | Deep texture on a *master* that still sticks | Named master barrier, then convert | Fast film in pockets; do not live in the cavity |
Silicone rubber already wants to stick to silicone oil. Spraying a dimethyl silicone aerosol into a silicone mold is how you get a permanently contaminated face.
Solvent sprays: what they do well and what they hide
They flash fast. They reach lettered texture on a rigid master better than a viscous water emulsion. That is why they stay on the *pattern* bench.
They also hide process problems. If the master is undercured SLA, the cavity is too rough, or the draft is missing, a heavy spray will still “release” while printing orange-peel and transferring to every dump. On platinum RTV, some sprays inhibit the surface. You get a sticky skin that looks like a material defect.
If you use a solvent spray on a master, apply a mist from a distance, let it flash fully, and wipe the excess off keys and the pour rim. A wet master is not a coated master. It is a puddle that will dump into the first pour.
Semi-permanent: leave it on the steel PO
The strip-to-bare-metal, thin coat, heat-cure, break-in sequence is how steel parts tools run. It is not how you maintain a culinary RTV tray. If a quote wants to “semi-permanent your gummy mold,” they are describing the wrong object.
Culinary and skin-contact cavities are a contamination topic
A chocolate mold, a muffin pan, a gummy tray, or a prosthetic pour face is a contact article. A solvent spray is not an ingredient. If any release is used, it has to be a grade whose composition is permitted for that contact, applied so transfer stays within the finished-article test, and the article must be tested *with that process aid present*. In practice, the cleaner path is: polish the master, draft, jacket, and peel so you do not spray the cavity.
Do not recommend a hardware-store silicone aerosol on a culinary cavity. Do not “burn it off in the post-cure oven” and call the mold food-grade. Residual oil will show in sensory tests and in 21 CFR 177.2600 extractives.
Common mix-up: spraying the RTV face because an LSR SOP said so
LSR into polished steel is often designed to run dry; if a film is used it sits on steel. RTV copies a master. Oil in the copy is in every dump. Same word “release.” Different face.
What to ask when you're buying
- Where does release live: master, cavity, or neither?
- Food or skin contact — is any film in the article test?
- Platinum inhibition plan for printed masters (barrier coat, UV post-cure)?
- Ban on sacrificial spray in culinary cavities, in writing?
- If they propose semi-permanent, are they quoting steel parts?
Worked example: 12-cavity chocolate bear
12-cavity, 18 mm, platinum 10A–20A, jacket. Master CNC, barrier-coated, no cavity spray. First dumps should peel from gloss without aerosol. If a bear locks, the geometry is undercut or you stripped too cold, not missing spray. A can on that face is a sensory and extractives problem.
When this article is the wrong quote
If you need semi-permanent on a hot HCR or LSR *parts* tool, send the parts OEM. A tiny shallow ice tray can skip film and jacket. Geometry can override: a locked soap dragon still wants peel and a shell, not more oil.
Related reading: FDA/LFGB food molds, cleaning culinary RTV, how to improve release, custom RTV molds.
Put this on the RFQ
“No sacrificial mold release on food-contact or patient-contact RTV cavities. Master barrier named if used. Semi-permanent only if this is actually a steel parts tool on a different PO.” That sentence prevents a well-meaning setup spray from becoming your contamination source.
Send the media (chocolate, pectin, resin, soap) and whether the cavity is the food/skin article. We will put barrier on the master and keep oil out of the pour.
We would not recommend a hardware-store aerosol in a culinary cavity
We would not recommend baking oil off and calling it 177.2600. We would not raise Shore A first to skip draft. We would not coat an RTV skin with a steel semi-permanent system. We would not treat stick in one pocket with a global spray.
RUUIPON Mold Structure Decision: peel path first. Flat back? open-back. Deep undercuts that cannot peel? two-part / plug / core, not more oil. Soft wet dump? mother mold. Stick in one letter is a master or draft problem.
- Master-to-RTV? - yes -> Named barrier on master; UV post-cure
- Master-to-RTV? - no, casting-to-cavity -> Food or skin?
- Food or skin? - yes -> No spray; fix peel/draft/jacket
- Food or skin? - industrial resin -> Minimal named film if plaque-tested
- Where does it stick? -> Quote says semi-permanent?
- Quote says semi-permanent? - steel parts tool -> Different an HTV product or mold RFQ here, or ask us if you need a high-volume LSR cold-runner tool PO
- Quote says semi-permanent? - RTV skin -> No spray; fix peel/draft/jacket
Typical shop values
Reference values only. Confirm material-specific limits against the supplier’s technical data and agree project acceptance criteria before production.
| Item | Typical shop value | | --- | --- | | RTV mix | Platinum 1:1 or 10:1; vacuum degas | | Cavity Shore | 10A–20A with jacket | | Platinum shrink | About 0.1–0.3% after full cure | | Master barrier | Named coat after full UV post-cure of SLA | | Culinary cavity spray | None; article is the food-contact face | | Cloth check after setup dump | Dry cloth should not pick up oil |
FAQ
Why keep solvent sprays off culinary RTV cavities? A spray is not an ingredient. Transfer shows in sensory tests and in 21 CFR 177.2600 extractives. Do not burn oil off in a post-cure oven and call the mold food-grade. Polish the master, draft, and peel so you do not spray; if any film is used, it must be permitted, controlled, and tested on the article.
When does a semi-permanent coating belong on this PO? When the object is a steel parts tool, not an RTV skin. Extra material on metal does not bond if the tool was not stripped and heat-cured. Do not bake that system onto a 10A food tray.
Can a platinum RTV culinary tool run with neither spray? Often that is the intent. Glossy platinum peels wax and chocolate without aerosol. If a casting locks, the geometry is undercut or you stripped too cold. Unapproved release puts a new chemical into the food or 10993 file.
Why is spraying dimethyl silicone oil into a silicone mold a bad idea? Silicone rubber wants to stick to silicone oil. You contaminate the face, get fish-eyes, and create inhibition drama on platinum. For RTV mold-making, release usually belongs on the master, not in the rubber.
How does a 10-minute cloth check tell which film you are running? Dump a setup shot, wipe casting and cavity. Oil on the cloth is sacrificial transfer. Stick in one pocket only is local polish, draft, or inhibition; a global spray will mask it for a day. If food or skin-contact dumps are on the bench, change the tool design rather than the aerosol.
Custom silicone development · DFM & prototype support
CAD, drawing, photos or sample details