Send the failure photo first. We name the symptom, then we say recast, jacket, split, or redesign. RUUIPON does that intake in Bao'an, Shenzhen. If the tool is still in spec and you only need more copies, production is MOQ 20 per design after approval. If the pocket is wrong, a prototype after CAD lock is usually 3-7 business days.
This is not a twin of the defects blog. That article lists problems. This URL is the shop door: match the mark to a fix page, or send the file and the dump so we can quote the next tool.
Name the failure before you recast
Start with the mark, not a hardness chart. Each row opens the page that already owns that failure. Do not send us a new outline that clones those URLs.
| What you see | Check first |
|---|---|
| Tear on demold | Follow the tear path. Thin letter islands and mascot necks fail first. |
| Pits or bubbles on the face | Mold-side vs pour-side. Vacuum on the rubber does not fix a trapped dump. |
| Flash or step on a split | Keys, closure, and jacket. More Shore will not close a walking seam. |
| Tray sag or warped storage | Loaded edge sag vs a tool that was hung or folded. |
| Texture gone dull | Wear vs dirty face vs the master already being soft. |
| Resin stuck or stained wells | Inhibition, leftover film, and whether a patch will print. |
| Piece will not dump | Wet cavity, undercured dump, or a geometric hook. Not one spray. |
| Worn tool, reorder question | Repair, recast from the mother, or cut a new master. |
What to photograph
If you send this, we can name the family:
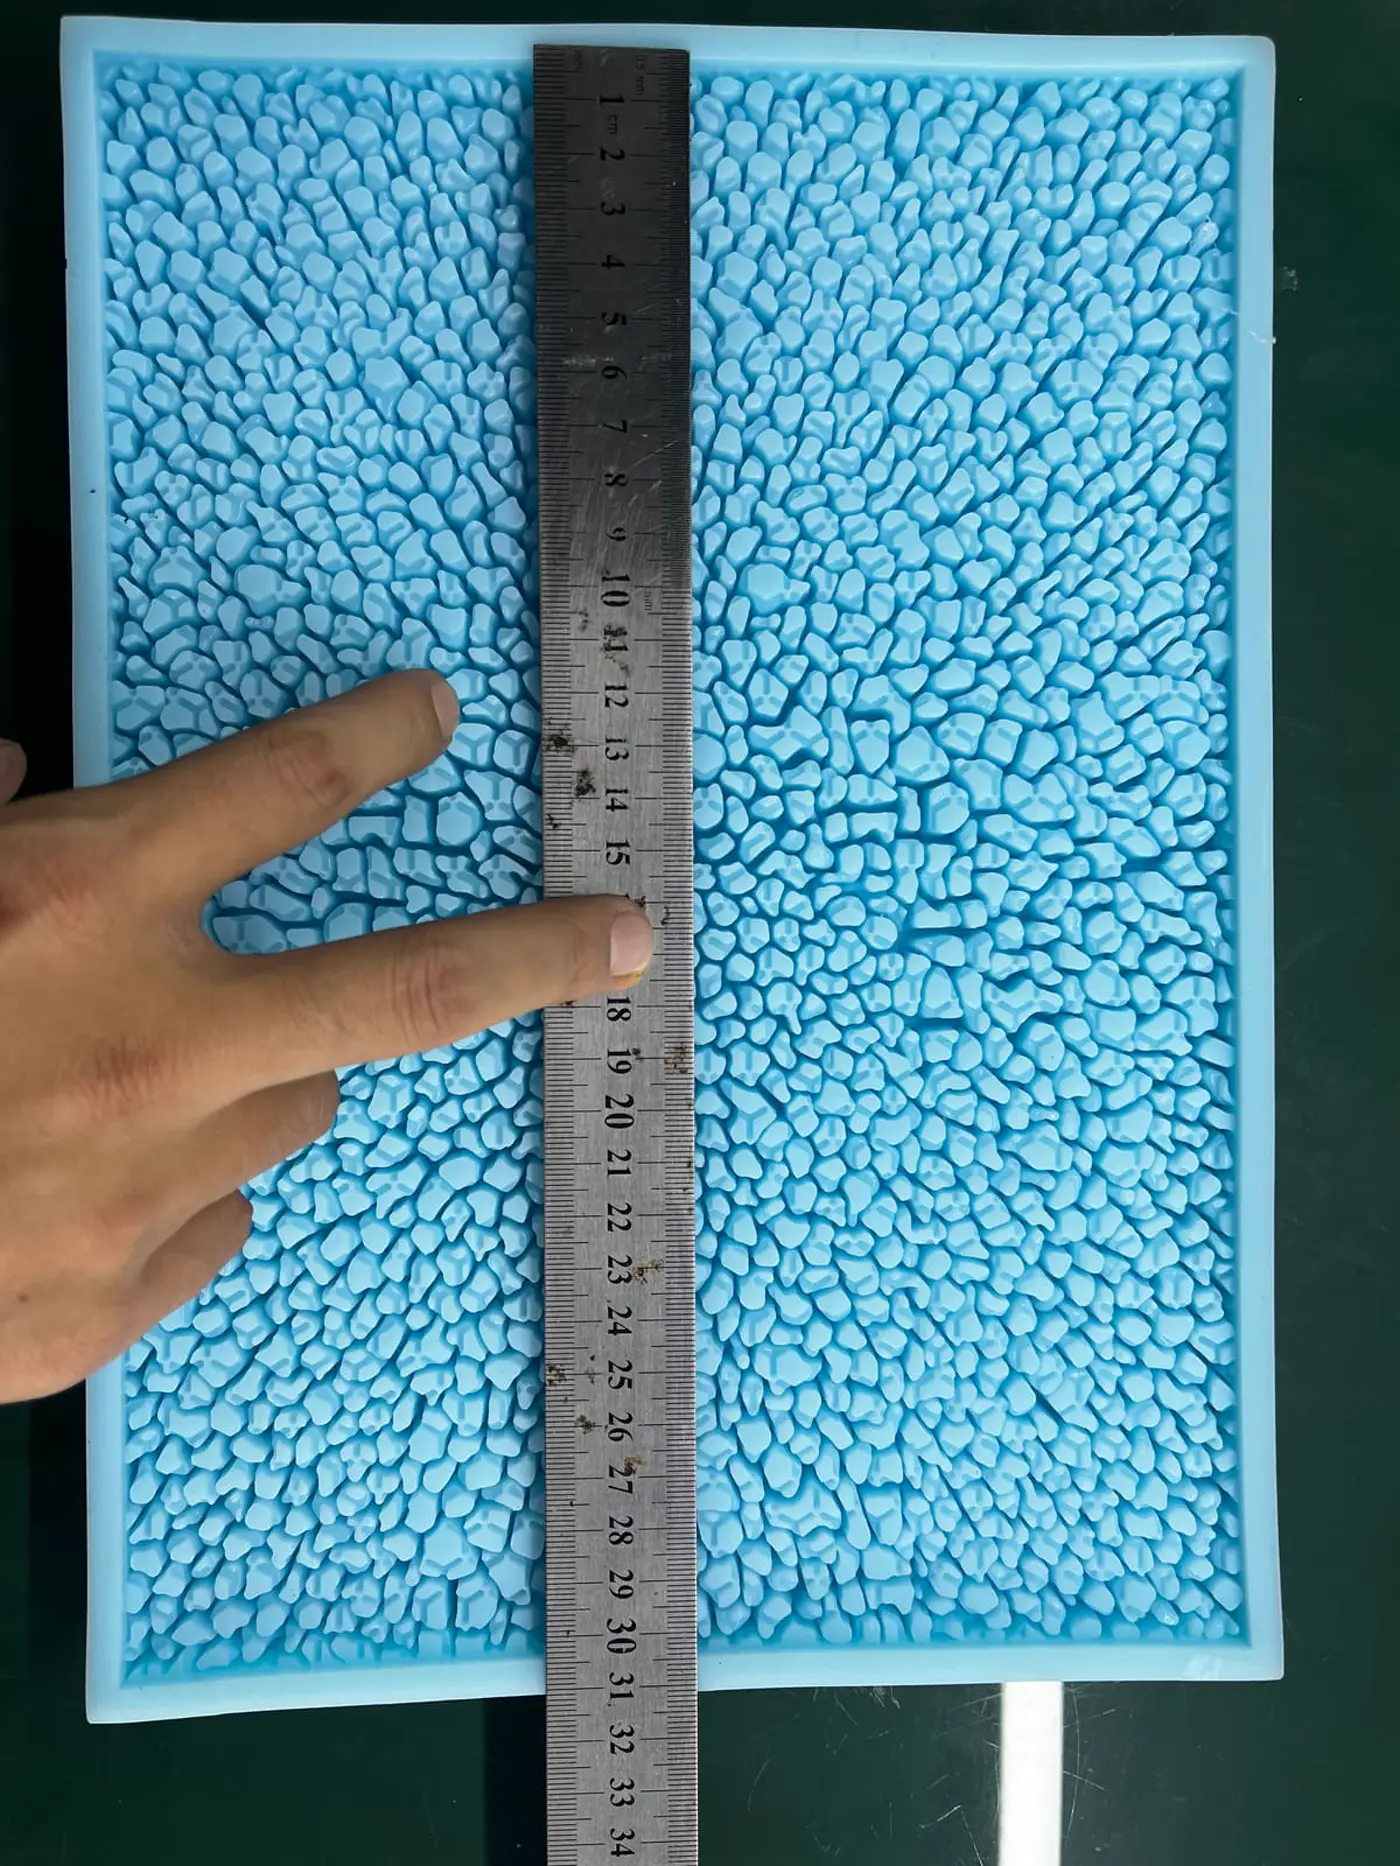
- the whole tray, dry, with a ruler in frame
- the bad cavity close-up, and one good cavity for compare
- the torn or flashed part, not only the rubber
- whether the mark follows the parting line
- what you poured, and about which dump number it started
We would not recommend recasting from a dim kitchen photo of a greasy tray with no dump named. That file gets a question list, not a PI.
Recast versus redesign
Recast when the resin production mother is still true and the rubber is what wore. Redesign when the tear, flash, or weight drift is in the pocket. A jacket (support shell) is a structure add, not a recast. Do not call the resin mother a mother mold.
If you only need more of an approved tool, say reorder. If the logo depth or cavity grams changed, that is a new CAD lock. Cost of a fresh tool sits on custom mold cost. A brand-new shape starts at custom silicone molds.
Worked example: pectin ear tear
Typical shop path, not a named customer. A 12-up bear dumped clean for a week, then the left ear tore on peel. The photo showed the tear starting at a 1 mm neck, not at a flash line. The dump was pectin, not gelatin. We would not have poured a 40A recast. We thickened the neck in CAD (USD $50 when that edit applies), locked the file, and prototyped in the 3-7 day window. MOQ 20 only after that peel passed.
FAQ
Can you tell what is wrong from one photo?
Often we can name the likely family: tear, flash, pit, sag, or stick. We still need the dump material and whether the mark follows the parting line. A dirty tray with no scale is not enough to recast.
Should I just order a harder Shore?
Not as the first move. A harder tray can hide sag and then tear a thin arm. We would not recommend changing Shore until the tear path and the dump are named.
Do you recast from the old mold?
We recast from the resin production mother when that mother is still true. Copying a torn RTV skin copies the tear. If the mother is lost, say so before we quote.
Is this the same as the defects blog?
No. The blog lists common problems. This page is the shop intake: send the failure, we point you to the matching fix URL or a recast quote. Production MOQ is still 20 pieces per design after approval.
New cavity, no failure yet? Use contact and name the dump. Already have a worn tray and a living mother? Say recast on the same form.