
RTV Mold Design for Grommet, Gasket, and O-Ring Casts
Production O-rings are a parts quote. An RTV analog is a casting cavity: split flash, jacket sag, peel through a membrane. Tool each geometry as its
 Kyler Yang · Founder10 min read
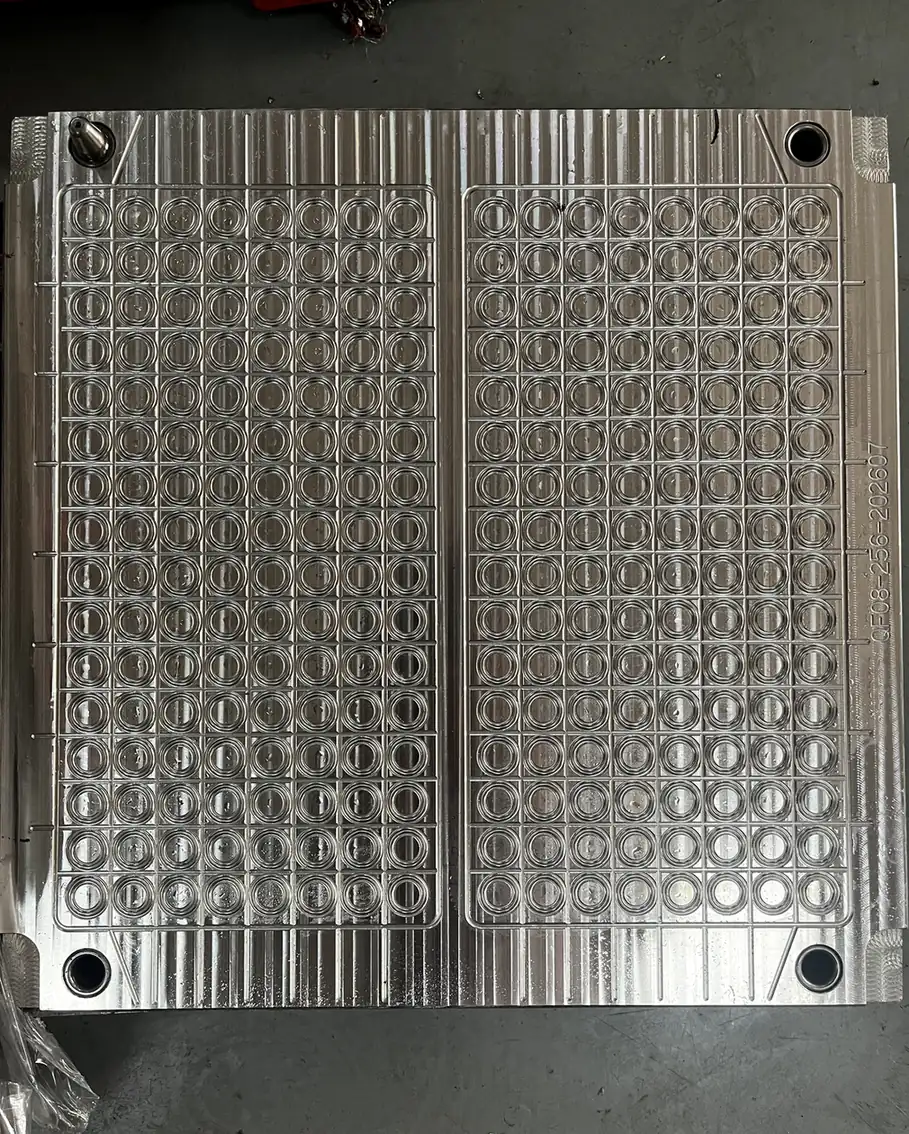
An O-ring *production* mold is a gland-and-flash problem on a LIM or HCR press. A gasket press tool is a land-and-set problem. A grommet steel tool is a stretch-through-hole problem. If you send all three to an RTV jacket shop as “a doughnut in rubber,” you will get a flexible cavity that dumps PU or wax — or you will get the wrong factory.
On this site the silicone is the cavity: resin master to RTV casting mold. You can pour short-run prototype seals, wax rings, or PU gaskets into that cavity. You cannot pretend a 10A–20A tray is an AS568 production cell. If you need thousands of vulcanized silicone O-rings, that is a different finished-part quote, often LSR with a cold-runner.
Name the part by how the *cavity* fails
O-ring casts. The functional surface is the torus. Flash at the RTV split becomes a leak path on the casting. Split placement and key quality dominate. Cross-section must be round after the pour, not oval from a jacket that pinched or a skin that took a set in storage.
Flat gasket casts. The functional surface is thickness. Jacket sag and pour-head variation dominate. A pretty edge with a thick flash skirt at the split is a scrap gasket even if it “seals on the bench” under extra bolt load.
Grommet casts. The functional features are the groove and the ID. Peel through a thin membrane, concentricity of ID to groove, and tear at the membrane dominate. Hardness that is right for an O-ring squeeze on a *part* is often too stiff to peel a grommet out of RTV — and too stiff to assemble if you cast a 70A copy in a 10A mold that flattered the stretch.
Write the failure mode on the mold kickoff. The split will follow that sentence.
Process choice before anyone cuts steel — or pours RTV
| Part | Default on this site | When to leave this site | | --- | --- | --- | | Prototype rings, wax, PU, resin seals | Platinum RTV, keyed split, jacket | Production silicone O-rings: LSR/HCR parts OEM | | Flat gasket layout checks | Open-back or two-part RTV; thickness is the jacket | Thousands of HCR gaskets: compression OEM | | Grommets with a thin membrane | Soft 10A–20A skin, peel path, maybe a core | Delicate high-volume LSR membranes: LIM cell |
Tin-cure RTV is a short-run or dirty-master prototype. It is not a production O-ring process, and it keeps shrinking on the shelf.
O-ring cavity rules (RTV analog)
Split line. Put it at the equator if you must split a two-part, and budget a defined, tiny flash you can destage. Better: a split that keeps the sealing bands free of witness. A longitudinal flash across the sealing line is a leak on the casting.
Keys and jacket close. Compression O-ring *steel* lives on land width. RTV lives on keys that return the halves to the same shut every pour. Too little close, flash. Too much squeeze on a soft jacket, the cavity loses roundness and you still flash at the corners.
Fill. Pour or inject the casting media so the last-to-fill is a non-sealing region. Avoid a sprue scar on the torus. Vacuum degas the *mold rubber* when you make the cavity; vacuum the casting if the media needs it.
Shrink and storage. Platinum RTV shrinks about 0.1–0.3% after full cure — not the 2–3% LSR *part* band. Do not paste LIM shrink onto the master. Post-cure the *casting* if that spec requires it, on a mandrel so rings do not oval. Loose rings in a hot pile come out egg-shaped. The mold itself should sit in its jacket so the torus does not take a set.
Finish. A smooth torus demolds and inspects cleanly. Texture is rarely useful on an O-ring. Do not polish only one half of the master; mismatch shows as a step.
Gasket cavity rules
Thickness is the seal. Call a thickness class that matches ISO 3302-1 (M2 is a common default unless the drawing says M1/M3) on the *casting*, then tool the jacket to hold it. A ±0.3 mm rubber title block on a 1.5 mm gasket is a shrug, not a spec. ISO 3302-1 is a drawing class, not “precision.”
Crush beads. If the gasket uses a molded bead, flash next to the bead is a shunt. Vent or overflow away from the bead, not across it.
Bolt holes. Molded holes need a peel path and enough rubber that the hole does not tear on demold. Punched holes in a flat sheet are a different process.
Do not “make it thicker” in the RTV cavity as a substitute for a low-set *part* grade. Extra thickness at the same bolt length is extra squeeze and more set — on the casting, on a parts quote. Here, extra thickness is often jacket sag.
Grommet cavity rules
Membrane thickness. The panel groove creates a thin web. If that web is too thin for the hardness you will *cast*, the RTV will still copy it and then the casting will tear on peel or at the customer. If it is too thick, the grommet will not seat. Prototype in the production hardness of the *casting*, not only in a soft RTV that flatters assembly.
Undercuts. Grommets are undercuts. RTV needs a peel, a split, or a removable core. Forcing a 70A cast off a solid core is a tear generator. The mold rubber can be 10A–20A; the article compound is a different SKU.
Concentricity. Cable ID to panel groove must be concentric. Tool the core from one datum. Do not accept a two-piece core that can shift with flash at the split.
Eject analog. You do not fire pins through an RTV membrane. You peel. Pins on a master that print into a sealing lip are leak paths on the casting.
Common mix-up: tooling a grommet like an O-ring doughnut on a LIM RFQ
Hardness that is right for O-ring squeeze is often too stiff to assemble a grommet — and a LIM cold-runner quote will not dump PU into a jacket. Name the object: cavity you pour into, or vulcanized silicone component.
What to ask when you're buying
- Is the silicone the cavity (RTV) or the seal (HCR/LSR)?
- Split location, shown, and keys in the jacket?
- Casting media, Shore of the *article*, Shore of the *skin*?
- ISO 3302-1 class on the casting, not “precision”?
- Who owns the master if we recast after a split change?
Worked example: 50 PU prototype rings vs 50,000 LSR O-rings
Buyer wanted Ø25 mm CS 2.5 mm rings, about 50 prototypes in PU, then 50,000 silicone rings a year. First object: keyed two-part platinum RTV, 10A–20A, jacket, split off the sealing band. Second object: LSR family tool, cold-runner, different quote. Same “O-ring mold” email.
When this article is the wrong quote
If you need production silicone O-rings, gaskets, or grommets in the thousands, send the parts OEM. A tiny open-back washer can skip a heavy jacket. Geometry can override quantity: a one-off deep-undercut grommet is still RTV at 20 casts.
Related reading: what RTV tooling means, flash at the RTV split, compression set of stored skins, custom RTV molds.
Drawing notes that save a recast
- Object: RTV cavity for [PU/wax/resin], not LIM
- Split location, shown
- Skin Shore (often 10A–20A) vs article Shore
- ISO 3302-1 class on the casting
- Finish on sealing faces versus other faces
- For grommets: panel thickness range and cable OD range
If those notes are missing, the mold shop will optimize for easy peel. Easy peel is not a seal.
Send the gland or flange drawing, media, and quantity band. We will say RTV split-and-jacket, or tell you the doughnut belongs on a parts RFQ.
We would not recommend a one-piece glove for a sealing torus
We would not recommend raising Shore A first to “stop flash.” We would not paste 2–3% LSR shrink onto the master. We would not prototype a grommet only in soft RTV and freeze that membrane for 70A production. We would not put the split on the sealing band.
RUUIPON Mold Structure Decision: flat gasket back? open-back. Torus or groove that cannot peel? two-part / core. Soft skin plus a wet pour? mother mold. If the silicone *is* the O-ring leaving a hot tool, stop.
- Vulcanized silicone part at volume? - yes -> finished-part HCR or LSR quote
- Vulcanized silicone part at volume? - no, short-run cast -> RTV cavity
- RTV cavity -> Geometry?
- Geometry? - flat gasket -> Open-back or two-part; jacket holds thickness
- Geometry? - torus -> Split off sealing band; keys
- Geometry? - grommet membrane -> Peel path or core; prototype in article Shore
Typical shop values
Reference values only. Confirm material-specific limits against the supplier’s technical data and agree project acceptance criteria before production.
| Item | Typical shop value | | --- | --- | | RTV skin | Platinum 1:1 or 10:1, 10A–20A, jacket | | Platinum shrink | About 0.1–0.3% after full cure | | Contrast: LSR *part* shrink | About 2–3% — do not put this on the master | | Contrast: HCR *part* shrink | About 1.5–2.5% — different RFQ | | ISO 3302-1 on the casting | M2 common default unless drawing says M1/M3 | | Static squeeze band (article, not mold) | Often discussed ~15–30%; do not invent it in the RTV cavity |
FAQ
Why can't I tool a production grommet like an RTV doughnut? An O-ring fails on flash and roundness in a gland. A gasket fails on thickness and set in a flange. A grommet fails on membrane tear, concentricity, and stretch through a panel. Production silicone seals are usually HCR or LSR parts. RTV is the short-run cavity.
Where must an O-ring split not sit on an RTV mold? Not as a longitudinal flash across the sealing contact bands. Equator split is a compromise with a defined tiny flash you can destage; better is a split that keeps those bands clean. A sprue scar on the torus is the same class of leak.
Why is gasket thickness the seal instead of a pretty edge? The face is squeezed a designed amount. A thick flash skirt is scrap even if extra bolt load "seals on the bench." Call a real ISO 3302-1 class, overflow away from a crush bead, and do not substitute extra thickness at the same bolt length for a low-set part grade.
Why prototype a grommet in the article hardness, not only soft RTV? Soft RTV flatters assembly. The panel groove is a thin web that will copy and then tear if it is too thin for that Shore A. Too thick and it will not seat. Peel on a thick shoulder; do not print master pins on a sealing lip.
What drawing notes stop the shop from optimizing only for peel? Object (RTV vs LIM), shown split, skin Shore vs article Shore, ISO 3302-1 class, finish on sealing versus other faces, and for grommets the panel thickness range and cable OD range. Easy peel is not a seal.
Custom silicone development · DFM & prototype support
CAD, drawing, photos or sample details